Адрес
No. 1 Yudong Road, Huishan District, Wuxi City, Jiangsu. 214103
Рабочие часы
Понедельник Пятница: 9AM - 5PM
Суббота: 9AM - 4PM
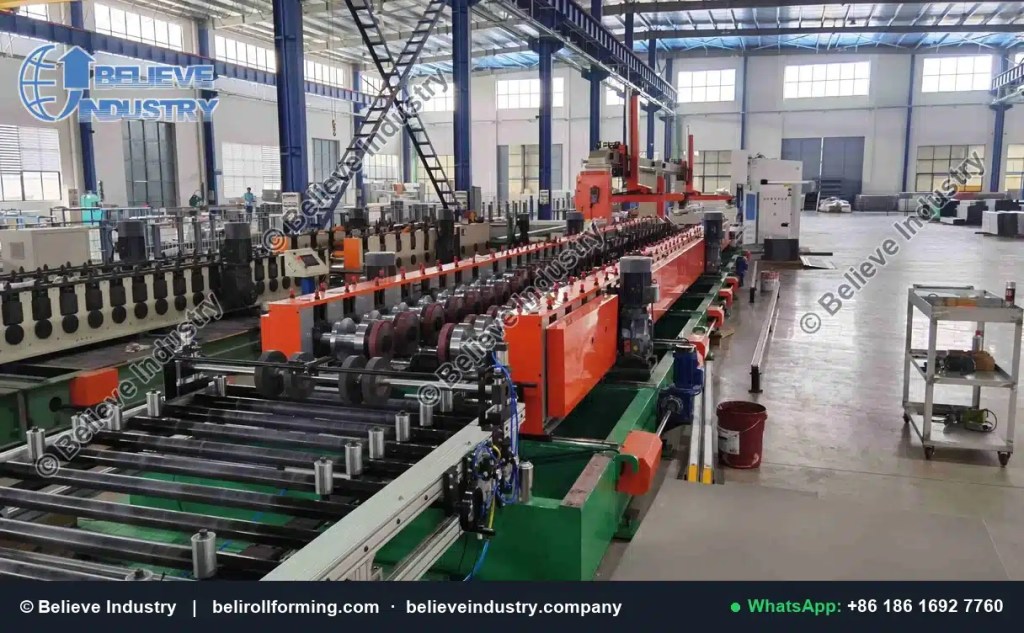
A cable tray machine upgrade rebuilds the weak stations of a line you already own. The usual scope is a servo punch press, a flying cut off, an automatic stacker and new controls. Budget runs 80,000 to 150,000 USD, output rises 25 to 40 percent, and payback lands in 12 to 18 months.
A cable tray machine upgrade only pays when the frame, the stands and the shafts are still sound. If the line was built for 1.2 mm strip and you now sell 2.5 mm tray, no retrofit saves it. The audit in step one decides that question before anyone signs a purchase order.
Most cable tray lines delivered before 2015 share one weakness. The punch press works in steps, so the line waits for the press on every pitch. The forming stands can run 25 m/min, and the press holds the same line to 3 or 4 m/min. A cable tray machine upgrade moves the bottleneck, and the bottleneck is where the money is.
A retrofit is a mechanical decision, not a budget decision. The table below is the screen we use on enquiry. Five of the seven rows point to an upgrade. Two of them point to a new line, and no supplier should talk you out of that.
| Situation on your line | Cable tray machine upgrade | New line |
|---|---|---|
| Frame and stands sound, 12 to 22 stands, shafts 60 mm or larger | Да | Not needed |
| Line built for 0.8 to 1.2 mm strip, you now need 2.0 to 2.5 mm | № | Да |
| Punch press limits the line to 3 or 4 m/min | Да | Not needed |
| Width change eats a full shift | Partial, with motorised width and recipes | Only if you need cassette speed |
| Cut length tolerance of plus or minus 3 mm, customer wants plus or minus 1 mm | Yes, with a flying cut off | Not needed |
| Three operators stacking by hand | Yes, with an automatic stacker | Not needed |
| Fewer than 10 stands or 50 mm shafts | № | Да |
The first question is shaft diameter. A 50 mm shaft carries a light section at low tension. Put a 2.5 mm trough with return flanges through it and the shaft deflects, the section opens, and the holes drift. A new stand set costs more than the rest of the upgrade combined, and that is where a new line wins.
The second question is stand count. A shallow C channel tray needs 12 to 14 stands. A perforated trough with return flanges needs 18 to 22. If your line has 12 stands and the new tray needs 20, a cable tray machine upgrade cannot add stations into a frame that has no room. Our guide to what a cable tray roll forming machine is sets out station counts per tray type.
A cable tray machine upgrade is modular. You can buy one step, three steps or all five. Each step has its own price band and its own effect on output. Prices below are 2026 shop figures for a line running 100 to 600 mm tray, and they exclude freight and civil work.
| Шаг | What changes | Typical price (USD) | Output effect | Line downtime |
|---|---|---|---|---|
| 1. Audit and baseline | Measurement, not hardware | 3,000 to 8,000 | None directly, protects the rest | Нет |
| 2. Servo punch and feeder | Hydraulic step press to servo press with servo feeder | 35,000 to 65,000 | Largest single gain, 30 to 50 percent | 3 to 4 days |
| 3. Flying cut off | Stop and cut to track and cut | 18,000 to 35,000 | Removes the stop at every cut | 2 to 3 days |
| 4. Run out and stacker | Manual stacking to automatic count and stack | от 15 000 до 30 000 | Frees 1 to 2 operators | 1 to 2 days |
| 5. Controls and recipes | Relay logic to PLC with stored recipes | 8,000 to 18,000 | Cuts changeover and scrap | 1 to 2 days |
The five steps overlap. A servo punch without a flying cut off still stops at every cut, so the punch gain is capped. A flying cut off without automatic stacking leaves the line waiting for a person at the end. That is why a cable tray machine upgrade sold as one package usually beats the same money spent on one large component.
Run the line for one full shift and record four numbers. Metres produced. Minutes stopped and why. Metres scrapped. Punches per minute actually achieved. Most plants guess the bottleneck and guess wrong.
Take a perforated tray at 12 pitches per metre. A hydraulic press with a 1.2 second cycle gives roughly 4 m/min. A 0.8 second servo cycle gives roughly 6.2 m/min. The forming stands were never the limit. If the audit shows 3.5 m/min on a line rated 25 m/min, the press is the target and the cable tray machine upgrade should start there.
The audit also protects you. Without a baseline, no supplier can prove a 30 percent gain after the retrofit. With one, the acceptance test at the end of the project has a number to hit.
The servo press is the core of most retrofits. A servo motor drives the ram, so stroke, speed and dwell are programmable. The press can punch while the feeder indexes, and it can skip a pitch when a pattern needs it. Tonnage stays in the same range, 40 to 125 t for tray work, because the die decides the tonnage, not the drive.
Two details decide whether the retrofit fits. First, the die set must match the new press bed and shut height. Second, the feeder must hold pitch accuracy of plus or minus 0.1 mm at speed. A cable tray machine upgrade that keeps an old mechanical feeder will lose the gain in hole drift.
Die sets are per pattern. Ventilation slots, splice holes, mounting holes and rung holes all live in the die. Ask for the full die list in the quotation, and ask which dies from the old press can be adapted. Adapting a die is usually cheaper than a new die, but only if the shut height allows it.
A stop and cut unit halts the strip, cuts, then restarts. At 6 m lengths, that is a stop every 30 seconds at 12 m/min. A flying shear tracks the moving profile and cuts on the fly, so the strip never stops. Length accuracy improves from plus or minus 3 mm to plus or minus 1 mm on most lines.
Этот руководство по летучим ножницам explains the hydraulic and servo tracking options. For tray, a servo flying shear is the usual choice because tray lengths are long and the cut repeat is high. A cable tray machine upgrade that adds a flying shear but keeps a worn run out table will still mark the tray surface.
Manual stacking ties one to three people to the end of the line, and it caps output at whatever a person can lift. An automatic stacker counts lengths, forms a bundle and pushes it out on a pallet. For 3 m tray the usual bundle is 20 to 40 pieces, and for 6 m tray 15 to 25.
An automatic stacker is also a safety upgrade. Manual handling of 6 m hot dip galvanised tray is the most common injury point on a tray line. The galvanizeit handling guidance explains why coated tray marks so easily. For a plant running 6 m lengths, step 4 is often the first part of a cable tray machine upgrade to pay back. It removes labour and damage at the same time.
Stacking is where the line reveals its true capacity. If the stacker handles 18 m/min, a punch upgrade to 12 m/min is fully usable. If the stacker handles 8 m/min, the line will queue at the end and the gain shrinks.
Old lines change width with hand wheels and a tape measure. A new PLC stores a recipe per width and per hole pattern. The operator selects the recipe, the line sets punch positions and cut length, and the first piece confirms the setting.
Recipe control is where a cable tray machine upgrade touches the автоматическое изменение размера question. If you already have motorised width adjustment, a recipe layer removes most of the remaining setup time. If width is set by hand, the recipe saves the arithmetic but not the spanner work.
Budget two days of operator training before production restarts. A servo press that nobody trusts will be run in manual mode, and manual mode gives back the whole gain.
Be blunt with yourself about four limits. First, frame rigidity. A light frame twists under a heavier section, and no cable tray machine upgrade corrects that. Second, stand count and roll design. Missing stations cannot be added into a full frame. Third, shaft and bearing size. Thin shafts limit thickness and tension. Fourth, straightener capacity. A leveler sized for 1.2 mm will not flatten 2.5 mm coil, and unflat coil ruins hole position.
If two or more of those limits apply, compare a new line. The о стоимости линии для кабельных лотков sets out what a new line includes, so the comparison is like for like.
Most retrofits run in a planned shutdown of 5 to 8 days. The sequence below is for a full five step scope. Partial scopes compress it.
| Day | Работа | Выработка |
|---|---|---|
| Before shutdown | Pre assemble skids, test servo press, label cables | Line still running |
| Day 1 | Isolate, lock out, remove old press and feeder | Нет |
| Day 2 to 3 | Install servo press, feeder, align to the first stand | Нет |
| Day 4 | Flying cut off, tracking encoder, run out changes | Trial lengths |
| Day 5 | Stacker, controls, recipes, safety interlocks | Trial bundles |
| Day 6 to 7 | First article, tolerance check, operator training | Ramp up |
| Day 8 | Handover with signed acceptance record | Full output |
Lock out and tag out applies to every task in the table. The OSHA 1910.147 procedure is the reference most export buyers ask to see in the method statement.
Plan the shutdown around your order book, not around the supplier calendar. A tray plant that stops in its peak month loses more than the retrofit gains.
The arithmetic is simple and it is worth doing before the quotation arrives. Take a line at 4 m/min, one shift of 8 hours, 250 working days. At 70 percent availability that is 3,360 m per day, or 840,000 m per year.
A cable tray machine upgrade that lifts line speed to 6 m/min raises output to 1,260,000 m per year at the same availability. At a contribution of 0.60 USD per metre, the extra 420,000 m adds 252,000 USD a year. Against a 120,000 USD retrofit, payback is under six months.
Most real plants land between 12 and 18 months, because demand, not capacity, sets the extra metres sold. The formula still matters. It tells you the minimum volume that justifies the spend, and it shows which step buys the most metres for the money.
| Сценарий | Line speed before | After upgrade | Extra metres per year | Payback at 0.60 USD/m |
|---|---|---|---|---|
| Punch only | 4 м/мин | 5.5 m/min | 315,000 | 9 to 12 months |
| Punch and shear | 4 м/мин | 6.5 m/min | 525,000 | 10 to 14 months |
| Five step scope | 4 м/мин | 6.5 m/min plus 2 operators | 525,000 plus labour | 12 to 18 months |
The labour line is real money. Two operators at 6,000 USD a year each is 12,000 USD of cost removed, and that number arrives every year without a sales effort.
A cable tray machine upgrade fails on scope wording more often than on hardware. Six items belong in the contract.
Run the acceptance test on your own material, not on the supplier sample coil. Coil with heavy coil set or a different coating changes the result, and the argument afterwards costs more than the test. A cable tray machine upgrade with a clear acceptance target is easier to defend in month six, when the line has been through a busy period.
Q: How much does a cable tray machine upgrade cost?
Q: Can you retrofit servo punching onto an old cable tray line?
Q: How long does the line stay down during a cable tray machine upgrade?
Q: Will a cable tray machine upgrade improve cut length tolerance?
Q: Can an upgrade let me run wider or thicker tray?
Q: How do I know if my line is worth upgrading?
Этот cable tray roll forming machine product page lists delivered layouts with station counts. If the section itself is still open, the сравнение лестничных и перфорированных лотков settles the tray type first. For a retrofit quote, send four things: a photo of the line, the shaft diameter, the current metres per shift, and one dimensioned tray drawing with its hole pattern. Those four inputs are enough to price a cable tray machine upgrade without a site visit.
Последнее обновление: 2026-11-18
История изменений статьи
2026-11-18: Initial publication. Five step retrofit scope, decision table against a new line, downtime plan, payback arithmetic, contract items and 6 FAQ.
Триггеры следующего пересмотра
Servo press and flying shear prices move more than 10 percent; new cable tray machine upgrade project data from shipped lines; NEMA VE 1 or IEC 61537 revision; quarterly SERP check for the focus term.
Cable Tray Machine Upgrade: 5 Retrofit Steps That Lift Output...
Читать далееHow to Identify Your Pallet Rack Upright: 6 Punch Patterns,...
Читать далееPallet Rack Upright Profile Names Explained: Teardrop, Sammons, Step Beam...
Читать далееStep Beam Roll Forming Defects: Bow, Twist, and Beam Sag...
Читать далее