What Is an Upright Rack Column Roll Forming Machine?
An upright rack column roll forming machine is a cold forming line that turns steel coil into the front column of a pallet rack upright, punching the connector hole pattern inline before the formed profile is cut to length. The machine does two jobs at once. It wraps flat coil into a column section, usually 3, 4, or 5 inches wide, and it punches the holes that carry every beam connection the rack will ever make.
Upright rack column roll forming machine definition: a coil-fed roll forming line with an inline punch press, producing pallet rack upright columns in configurable widths and gauges, with hole patterns punched to a fixed pitch while the strip is flat.
Short answer: the hole pattern is the product. Teardrop punching dominates North American pallet racking on a 2 inch pitch and works with hook-type beam connectors under ANSI MH16.1. Keyhole punching serves European and light duty shelving on a 50mm pitch with drop-in connectors. Teardrop tooling costs more and wears faster on the irregular profile, but it opens the larger market. Most lines we build now punch teardrop on both column faces in one pass.
That is the whole argument in four lines. The rest of this page is the evidence, because buyers who choose a hole system without checking pitch tolerance, die economics, and connector supply end up buying a second punch unit two years later. Before we go deep, it helps to see how the punching unit sits inside the full línea de máquinas perfiladoras layout, since the punch is only one station among many.
The Hole Pattern Is the Product, Not a Detail
Buyers new to racking production compare column widths and gauges. Buyers who have run a rack factory compare hole patterns first. Every beam level in the finished warehouse hangs on those holes. Get the shape wrong and no connector on the market fits. Get the pitch wrong by a fraction of a millimetre and the beam still fits but the level is off, and the error compounds over 9 metres of column.
This is why the column line is really a punching machine with roll stands around it. The forming section is mature technology and every serious builder gets it right. Punch shape, punch drive, pitch control, and die life decide your scrap rate and your labour cost for the life of the line.
We have built rack column lines for more than 15 years and shipped them to over 20 countries. The single most common retrofit request is a punch unit upgrade, not a forming section upgrade. Choose the punching system like it matters, because it does. Our máquina formadora de rollos de bastidor vertical guide covers the base line architecture, and this page goes one level deeper on the hole question.
Teardrop Punching Explained
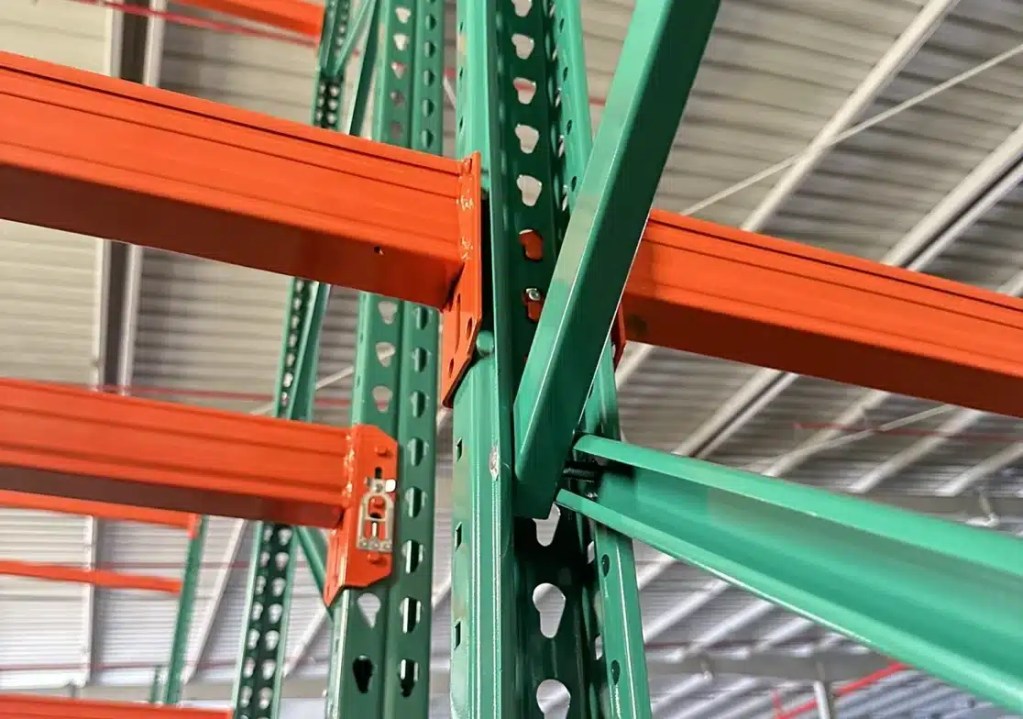
The teardrop is the standard connector hole of North American pallet racking. The shape is a circle merged with a tapered slot, wider at the top, so a teardrop connector drops in under gravity and rotates down into the round seat. No clips, no pins, no fasteners at the connection. Installers love it and that love is why it dominates tenders from Ohio to Ontario.
| Teardrop attribute | Typical value | Por qué es importante |
|---|
| Hole width | About 33mm at the round seat | Fits standard teardrop beam connectors |
| Pitch | 2 inch (50.8mm) | North American default, some tenders ask 1.5 inch |
| Punch force | Higher than round holes | Irregular profile concentrates load at the point |
| Compatible standard | ANSI MH16.1 (RMI) | The design code US and Canadian inspectors work to |
| Connector supply | Widest in the Americas | Every major beam maker stocks teardrop ends |
Two facts about the shape matter for tooling. First, the pointed profile is not friendly to the punch. A round hole distributes punching load evenly around the perimeter. The teardrop point concentrates it, so the die corner at the point wears first and the burr shows up there first. Second, the profile must be oriented the same way on every hit. Rotate the punch 180 degrees and you get a mirror-image hole that half the connectors will not seat in.
If your market is the Americas, teardrop is not one option among several. It is the default, and the Máquina formadora de rollos para estanterías de palés con forma de lágrima platform exists specifically to punch it on both column faces at full line speed.
Keyhole Punching Explained
The keyhole is a round hole with a narrower slot below it, the profile of an old keyhole. A connector with a hooked end drops through the wide part and slides up so the shank seats in the round section. The connection is positive, but assembly direction differs from teardrop and the connector family differs with it.
| Keyhole attribute | Typical value | Por qué es importante |
|---|
| Hole geometry | Round seat plus parallel slot | Suits drop-in hook connectors |
| Pitch | 50mm in European practice | Neighbours the EN 15512 design world |
| Punch force | Lower than teardrop | Symmetric profile, even load distribution |
| Common market | European shelving, light duty racks | Selective pallet rack uses it less |
| Costo de herramientas | Lower die complexity | Two simple profiles instead of a merged curve |
Keyhole earns its place in three situations. Light duty and medium duty shelving lines punching thinner material, where the connection loads are modest and die cost matters more. European-market export work, where customers check hole patterns against what their connector suppliers already stock. And mixed product lines that run shelving uprights and rack columns on the same mill, where the keyhole profile is already in the tooling drawer.
What keyhole does not buy you is the Americas pallet rack market. A US distributor asking for teardrop does not accept keyhole because it punched faster. Know your customer list before you let the tooling budget decide.
Teardrop vs Keyhole: Side by Side
The honest comparison comes down to market access, tooling economics, and connection behaviour. Here they are together.
| Factor | Teardrop | Keyhole |
|---|
| Dominant market | North America, Australia, Middle East tenders | Europe, Asia, light duty shelving |
| Standard pitch | 2 inch (50.8mm) | 50mm |
| Connector style | Rotating hook, drops in from front | Straight hook, drops and slides up |
| Punch load | Higher, point concentrates force | Lower, symmetric profile |
| Die complexity | Merged curve, orientation critical | Two simple profiles |
| Die life to first regrind | Shorter than round, watch the point | Longer, even wear |
| Design code fit | ANSI MH16.1 rack designs | EN 15512 rack designs |
| Retrofits in the field | Easy, connectors everywhere in NA | Harder in NA, common in EU |
One point on that table deserves emphasis because it decides more quotes than any other. Pitch is not the same as hole spacing tolerance. A 2 inch teardrop pitch and a 50mm keyhole pitch differ by 0.8mm per repeat, and a column with 200 holes accumulates that. A good upright rack column roll forming machine holds the pitch, not the hole count. You program pitch, so 2 inch and 50mm are both just numbers in the HMI. What you cannot program away is pitch error.
Fact: Pitch Accuracy Is the Tolerance That Decides Everything
Beam level accuracy is the sum of pitch errors below it. Column at level five sitting 3mm high sounds cosmetic until you stack a 12 metre column and the top hole pair will not accept the connector without a hammer. Installers remember factories whose columns need hammers. They order from somewhere else next year.
Practical numbers from the lines we commission. Pitch repeatability on a servo punch holds within 0.25mm hit to hit. Mechanical presses with a flywheel and pitch chain hold 0.5mm when fresh and drift with chain wear. Over a 9 metre heavy duty column at 2 inch pitch, that is roughly 177 holes, and drift shows up as cumulative length error, not as scattered misses. Cumulative error is the dangerous kind because it looks fine on any single hole.
The fix is encoder feedback on the punch stroke relative to strip position, plus a pinch roll that never lets the strip creep during the hit. Ask any vendor for the pitch error over a full 9 metre column, not the hit-to-hit figure. The difference between the two numbers is the difference between a machine that makes sellable columns and one that makes rework. The way forming and punching trade tolerances back and forth is the same theme we cover in Cómo funciona una máquina perfiladora, just at finer numbers.
Fact: Die Life Depends on Shape, Steel, and Alignment
Die life is where the teardrop vs keyhole decision gets expensive or gets cheap. Three variables dominate.
| Variable | Effect on die life | What to control |
|---|
| Hole shape | Teardrop point wears 2 to 3x faster than a round or keyhole profile | Die material at the point, regrind schedule |
| Steel yield and thickness | 550 MPa 4.0mm coil cuts die life roughly in half versus 2.5mm 340 MPa | Punch force headroom, proper clearance |
| Punch to die alignment | 0.1mm misalignment can halve die life and doubles burr height | Guided punch units, not open presses |
Concrete numbers. Tool steel dies punching 2.5mm medium duty teardrop at proper clearance typically run 80,000 to 150,000 hits before the first regrind, with the point corner going first. The same steel punching keyhole in the same gauge runs noticeably longer because the load spreads evenly. Carbide inserts at the point stretch teardrop die life several times over and pay for themselves on any line running heavy gauge columns two shifts a day.
Regrind discipline matters more than die brand. Track hits, pull dies on schedule, regrind 0.3 to 0.5mm off the face, and restore clearance. Shops that run dies to visible burrs pay for it twice, once in deburring labour and once in connector complaints from the field. If your business case hinges on punch die life, price the die package as a running cost per column, not a one-time line accessory. The general mechanics of why high yield steels punish tooling live in our conformado en frío descomponer.
Fact: Double Sided Punching Halves the Handling
Both faces of a pallet rack column need the hole pattern. Beam connectors engage the front face, and the back face carries the pattern for bracing, anchor plates, or a second connector family depending on the design. There are two ways to get there.
Single sided punching runs the column, flips it, and runs it again. That doubles handling, doubles the chance of a scratch on the finished face, and adds a second setup to hold in pitch registration. Shops running this way typically lose 15 to 20 percent of line output to the flip operation, and the flip is where columns get dented.
Double sided punching puts two synchronized punch units, one per face, in the same station. Both patterns register to the same strip encoder, so the front and back patterns stay locked to each other by construction, not by operator care. On a four inch teardrop column this is the standard configuration we ship, and it is the whole reason the dedicated tear drop pallet rack platform earns its keep. For factories planning a multi-spec column strategy, double sided punching is one of the features covered in our multi-spec upright column line guide, alongside the changeover economics.
Fact: Servo Punching Changed the Build-versus-Buy Math
Ten years ago the punch unit was a mechanical press with a die cluster and a pitch chain. Changing pitch meant changing chains or gears. The whole line was shaped around that limitation.
A modern servo punch treats pitch as a program value. Two inch, 50mm, 1.5 inch, or a customer’s odd pattern all live in the recipe list. The punch synchronizes to line speed, ramps down for short hole spacings, and marks each hit against the die life counter automatically. Maintenance gets real numbers instead of operator memory.
| Punch drive | Typical rate | Pitch change | Best fit |
|---|
| Mechanical press, pitch chain | 30 to 50 hits per minute | Chain or gear change, hours | One pattern, one market, forever |
| Servopunzón | 40 to 60 hits per minute, syncs to line speed | Recipe change, seconds | Mixed markets, export work, tenders |
The rate numbers look close, and they are. The case for servo is not raw speed. It is that a column line with a servo punch can quote a 50mm keyhole tender on Monday and a 2 inch teardrop tender on Wednesday without touching tooling pitch hardware. For a factory selling into more than one region, that flexibility is the difference between bidding and watching. Where budgets are tight and the market is single-pattern, a mechanical unit still makes sense, and our precio de la máquina perfiladora de rodillos guide shows where that trade lands.
Which System Should You Choose?
The decision tree is short. Answer these in order.
- Where do you sell? Americas, Australia, or Gulf pallet rack tenders point to teardrop. European shelving and light duty work points to keyhole. Selling into both? You need both patterns, which means a servo punch with two die sets.
- What gauge will you run? Above 3.5mm and 450 MPa yield, teardrop dies should be carbide at the point or you will regrind weekly.
- Do both faces need the pattern? Almost always yes for rack columns. Budget double sided punching from day one.
- Who supplies your connectors? Lock the connector drawing before finalizing the die drawing. Die to connector, never connector to die.
Most factories we quote end up teardrop-forward, because North American pallet racking and Gulf tender work keep the line fuller than anything else, and because the connector supply chain in those markets is the deepest in the world. The code context behind that, ANSI MH16.1 as maintained by MHI, and the European counterpart EN 15512, are worth reading before your first tender response. Material choice interacts with all of this, and our máquina perfiladora de rodillos personalizada page covers lines built around a specific market’s hole pattern from the start.
One last opinion from the commissioning floor. Buyers who agonize over punch shape and then accept the cheapest cutoff saw have their priorities backwards. A crooked cutoff ruins a column with perfect holes. The punch and the cutoff are a pair. Spec them together, and if you want to see the finished columns in context, the máquina perfiladora de estanterías para palets page shows the full component family a single factory typically produces.



 English
 Español
 Português
 Русский
 العربية
 Bahasa Melayu
 Türkçe
 ไทย
 Bahasa Indonesia


